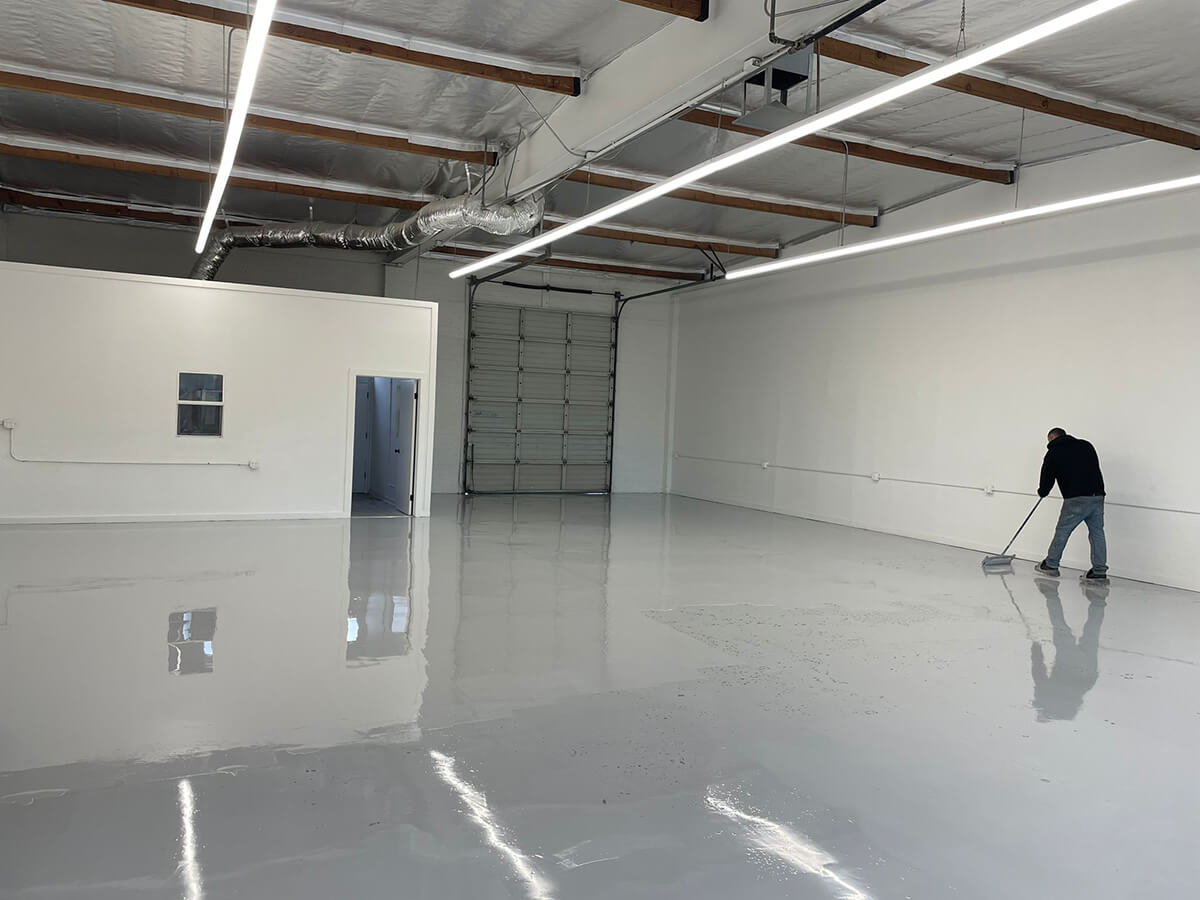
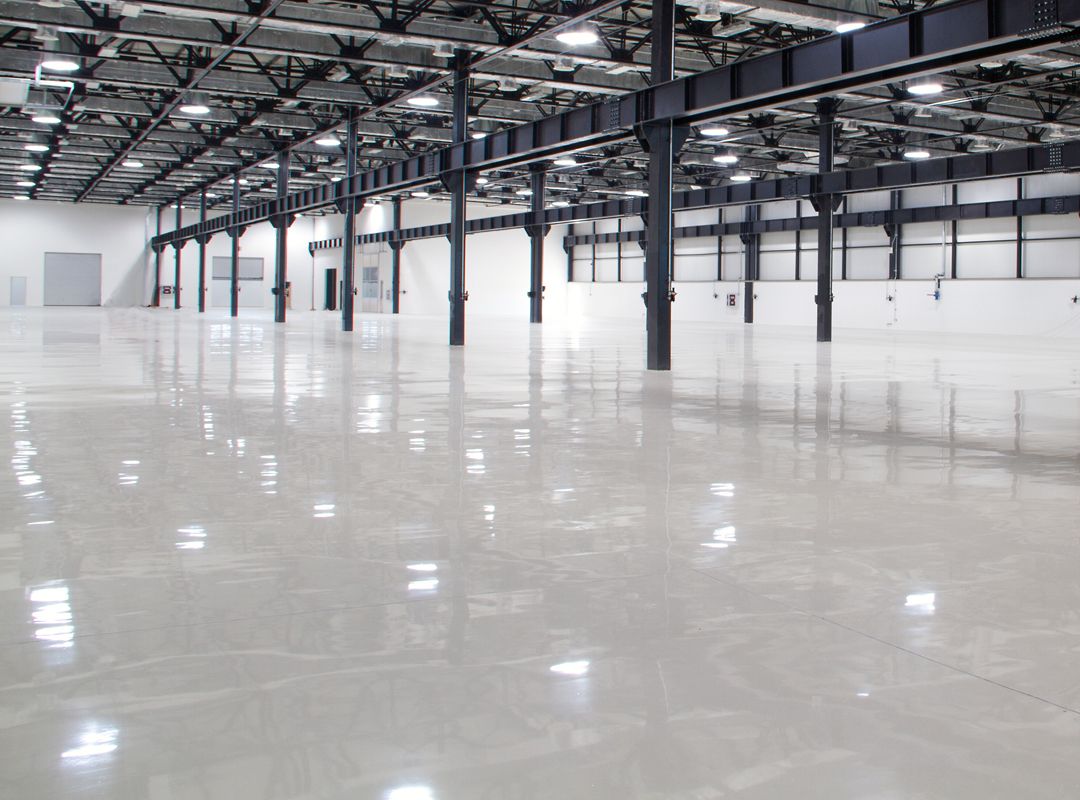
When a coating peels, the first instinct is to blame the material. In our experience that is almost never the culprit. The coating failed because it never had a mechanical key into the concrete in the first place.
Preparation is the least visible and most expensive part of a coating job, which is exactly why it is the part that gets cut when a bid needs to look cheaper.
What a surface profile actually is
Concrete Surface Profile, or CSP, is an industry scale describing how rough a prepared slab is. A polished, closed slab is effectively CSP 1. An aggressively shot-blasted floor might be CSP 5 or higher.
Every coating system has a CSP range it is designed to bond into. Apply a high-build system to an under-profiled floor and it will sit on top of the concrete rather than grip into it. Adhesion becomes a matter of surface tension, and surface tension loses to a forklift.
Acid etching is not preparation
Acid etching opens the surface chemically, leaves behind salts that must be fully neutralized and rinsed, and produces an inconsistent profile that is rarely adequate for a commercial system.
It also introduces water into the slab right before you seal it. We do not use it on commercial work, full stop.
Free assessment
Not sure which system your facility needs? We will walk the floor, test the slab, and give you an itemized proposal at no cost.
Request a Free QuoteDiamond grinding versus shot blasting
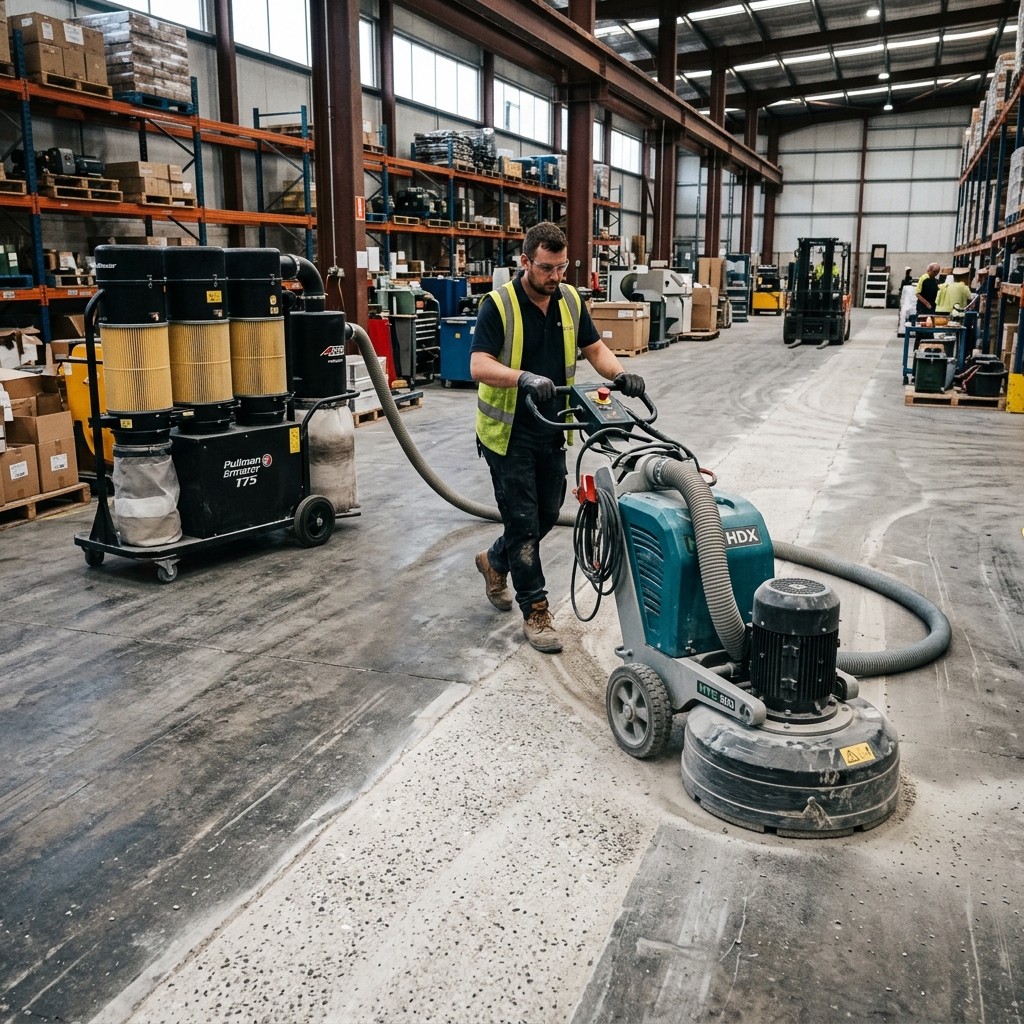
Planetary diamond grinders remove contamination and previous coatings while producing a consistent, controllable profile. They run with HEPA dust extraction, which matters in an occupied building.
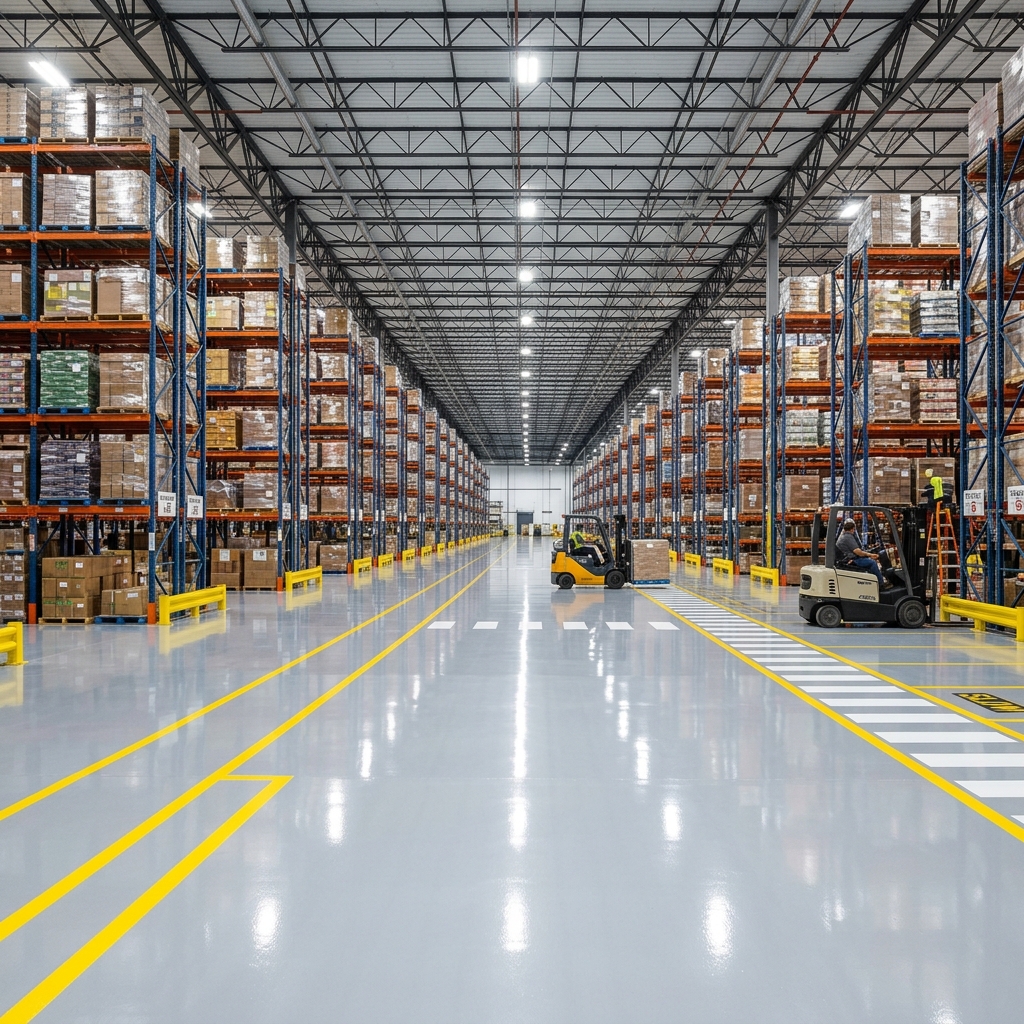
Shot blasting is faster over large open areas and produces a more aggressive profile, making it a good fit for high-build systems in big warehouses. It is less precise near walls, equipment and detail work.
Most of our projects use both: shot blasting for the open field, diamond grinding for perimeters, transitions and detail.
The steps that never get skipped
Whatever the building, the preparation sequence follows the same order.
- Moisture vapor emission testing before anything is specified
- Removal of all existing coatings, sealers, curing compounds and contamination
- Mechanical profiling to the CSP range the system requires
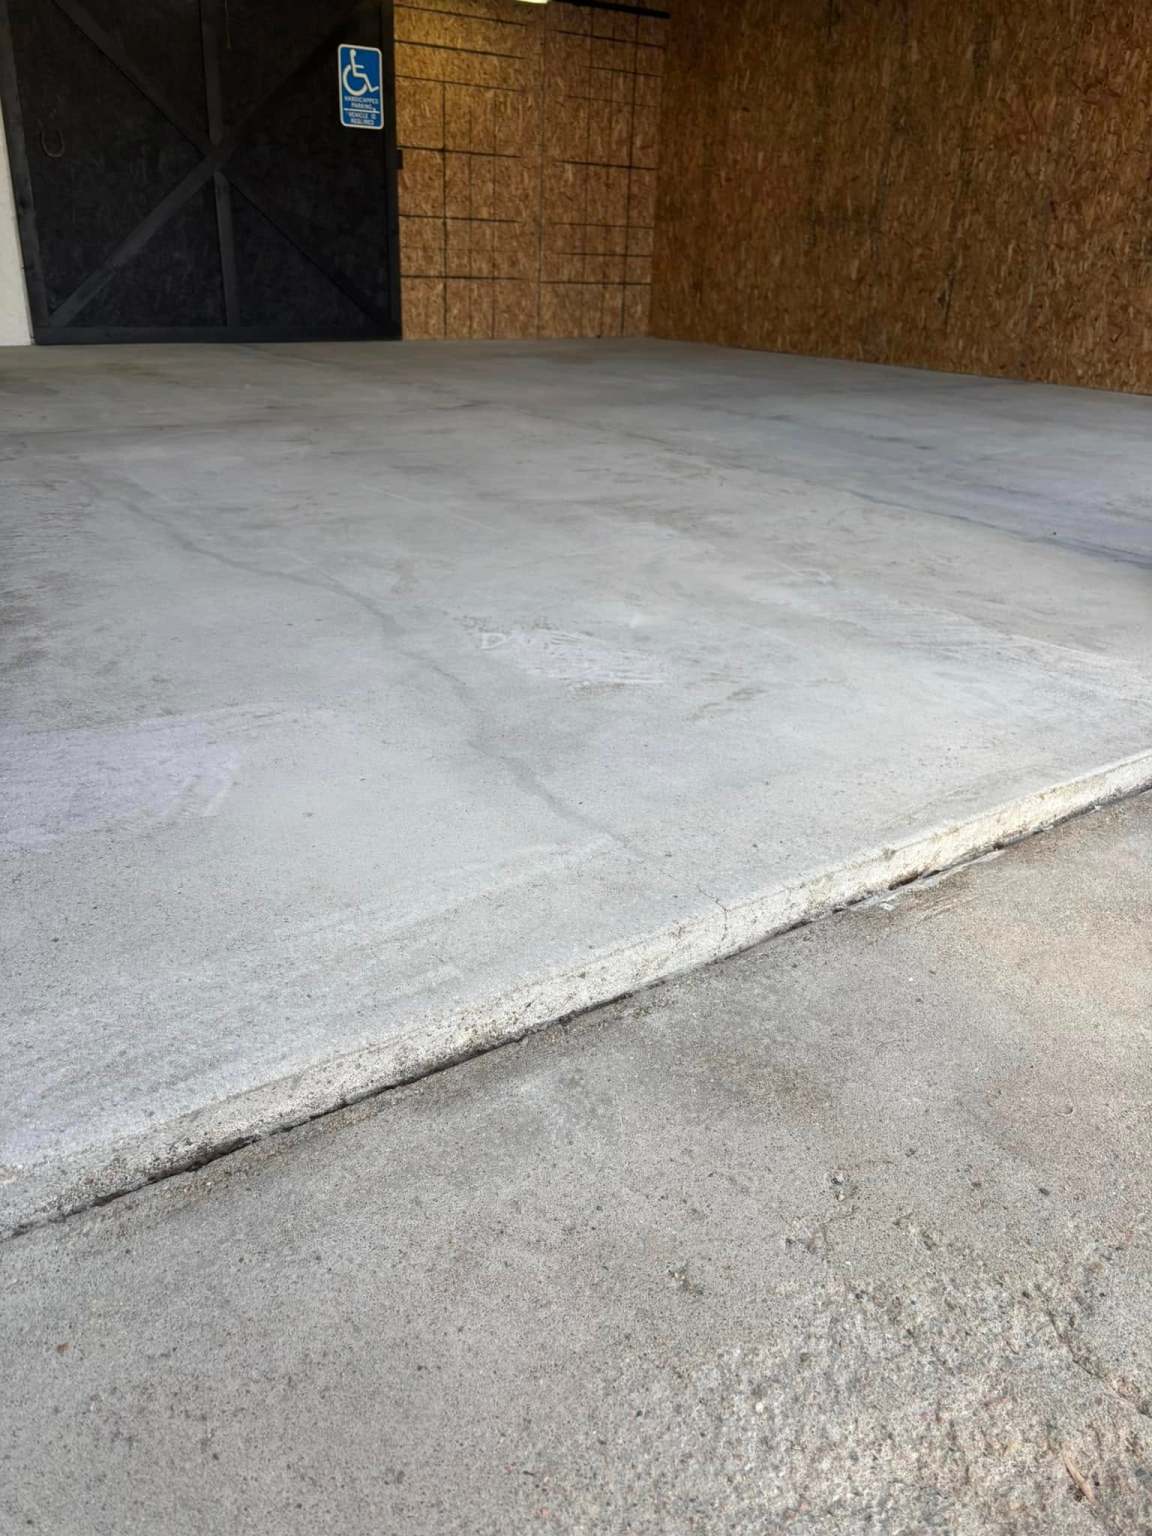
- Crack, spall and joint repair with the correct structural materials
- Full HEPA vacuum and inspection before the first coat goes down